

Tunnel freezerSKT
01/1800/2950




Basic data
- Machine type:
- Tunnel freezer
- Manufacturer:
- SKT
- Model:
- 01/1800/2950
- Year of construction:
- 2001
- Condition:
- good (used)
- Functionality:
- fully functional
Price & Location
- Location:
- 3e Loosterweg 40, 2182 CV Hillegom, Netherlands
Technical details
Dimensions and weight
Accomodation and amenities
Details about the offer
- Listing ID:
- A23363122
- Reference number:
- 18627
- Update:
- 20.11.2026
Description
Itjdpj Ak Uvwjfx Anwep
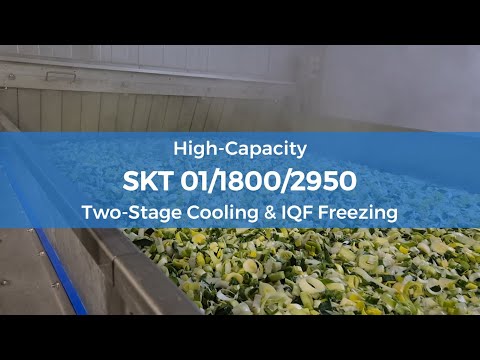
The freezer operates using a two-stage cooling process, consisting of an external infeed conveyor, a precooling section inside the freezing cell, and a long freezing tunnel equipped with high-capacity evaporators. This staged approach ensures controlled temperature reduction, optimal airflow, and uniform freezing conditions throughout the process.
Products enter the processing line via the external infeed conveyor at an approximate temperature of +40 °C. From there, they are conveyed directly into the precooling section located inside the freezer cell. The infeed conveyor has a total length of 3000 mm, ensuring a smooth and continuous transfer of the products from the ambient environment into the controlled freezing area.
Stage 1 – Precooling Section (Inside Cell) In the precooling section, products are conveyed on a stainless-steel belt with a length of approximately 9,350 mm and an infeed height of 3750 mm. During this stage, the product temperature is gradually reduced from +40°C to +10°C, ensuring a controlled cooling process before deep freezing. The section operates at an evaporation temperature of –2°C and is equipped with two evaporators providing a combined cooling capacity of 700 kW. This controlled precooling step minimizes thermal shock and prepares the product for efficient freezing in the tunnel.
Stage 2 – Freezing Tunnel After precooling, products enter the main freezing tunnel, where they are frozen from approximately +10°C down to a core temperature of –18°C. The tunnel features a stainless-steel conveyor belt with a total length of approximately 21,450 mm, providing sufficient residence time for complete freezing. This section operates at a low evaporation temperature of –40°C and is equipped with seven evaporators delivering a total cooling capacity of 2,100 kW. At the entrance of the freezing zone, a stepped conveyor belt ensures optimal product separation, maximized airflow, and efficient heat transfer, resulting in uniform IQF performance. When the product is frozen to a core temperature of -18°C the products leaves the belt at a height of 2750 mm.
To maintain consistent capacity and operational efficiency, the tunnel freezer is equipped with an automatic defrosting system. This system includes two freezing doors per evaporator: one located at the air inlet and one at the air outlet of the evaporator coil. During the defrost cycle, the doors automatically slide into position, isolating the evaporator and preventing cold air from passing through. Hot gas defrost is then activated, allowing accumulated frost and ice to melt. The resulting water is collected and discharged through a dedicated drain system to the outside of the tunnel. Defrosting time and cycle settings are fully adjustable via the PLC control system, ensuring optimal performance under varying operating conditions.
Supplied with original electrical cabinets, the SKT freezer features twelve Mitsubishi A500 and two A800 frequency converters, providing precise motor control and full process flexibility. Belt speeds, airflow, and other parameters can be easily adjusted to match product requirements.
Seller
Last online: Today
Registered since: 2012
41 listings online
Send inquiry
Telephone & Fax

Machineseeker Trust Seal
What is the trust seal?
Machineseeker certifies selected sellers with the Machineseeker trust seal. Before approval, a standardized and comprehensive check is carried out by experienced Machineseeker staff.
What do we verify?

Check of
trade licence or commercial register extract
Verification of the dealer's
postal address
Validation of the
banking details
Verification of
accessibility to
main phone number
Credit report
may not contain negative criteria
Buyer complaints
can lead to withdrawal of the sealWhat does this mean for you as buyer?
The Machineseeker trust seal enables you, as a buyer, to identify trustworthy sellers who are very likely to do honest and righteous business, without having to do your own investigation.
Disagreements may of course still arise during the purchasing process. Machineseeker is not liable for any legal violations by buyers or sellers active on Machineseeker.